
Problem statement: why this feels urgent on the factory floor
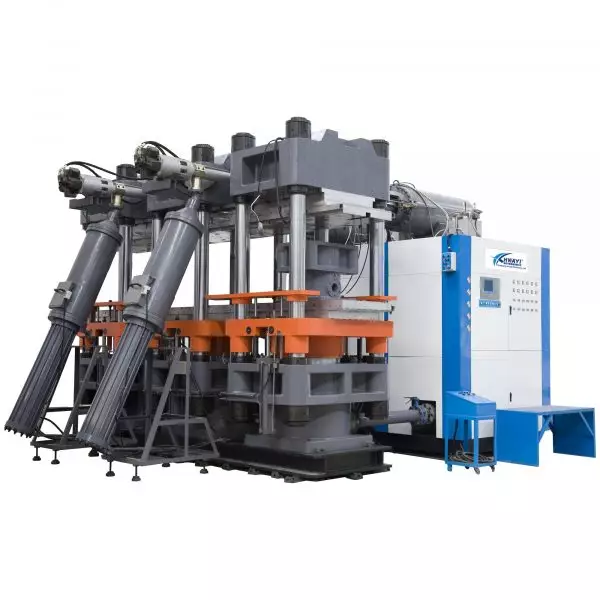
The station hums like a small engine room aboard a starfreighter—pressure gauges climb, seals sweat, and an unseen force concentrates at a single point: the hydraulic manifold. High-pressure hydraulic failures in vulcanizing lines produce energy release comparable to a mechanical pulse, and when a operator’s hand or a die set sits in the wrong place, damage escalates instantly. A practical fix begins with recognizing the failure modes in plain terms—hose burst, seal failure, valve stick—and proceeds to systemic cures. Early detection matters; today’s retrofit sensors and conditioned monitoring are the difference between a near-miss and a lost shift. Consider how a modern c frame rubber injection molding machine integrates into a cell: its cycle timing and pressure profile must be treated as part of the safety system, not merely production data. c frame rubber injection molding machine
Root causes mapped like a star chart
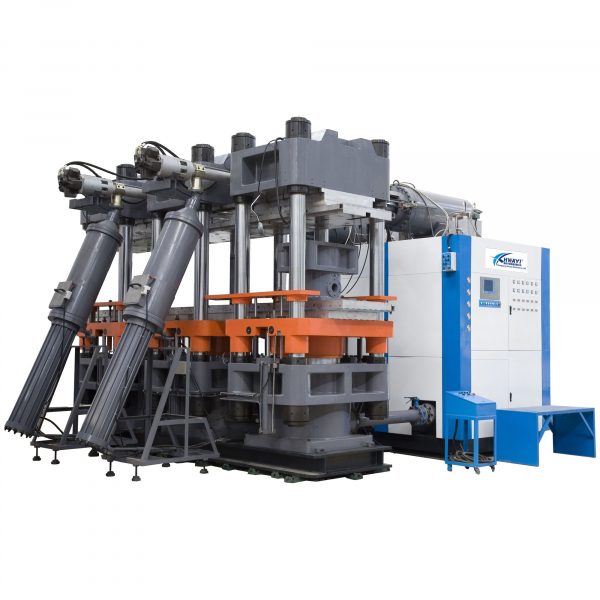
Hydraulic hazards rarely arrive alone. They form from combinations: aged hoses under cyclic fatigue, incorrect pressure relief settings, operator bypasses of interlocks, and poor isolation during maintenance. In one Akron, Ohio rubber plant, engineers traced repeated seal failures to a misadjusted presetter and a mismatched relief valve—the small details that produce catastrophic energy release. The technical vocabulary here—pressure relief valve, backflow valve, transfer molding interface—maps directly to inspection checklists. Fix any one of these and the system remains fragile; fix the combination and the workstation stabilizes.
Three-tier mitigation framework every safety officer should know
Think in layers: containment, control, and cognition.
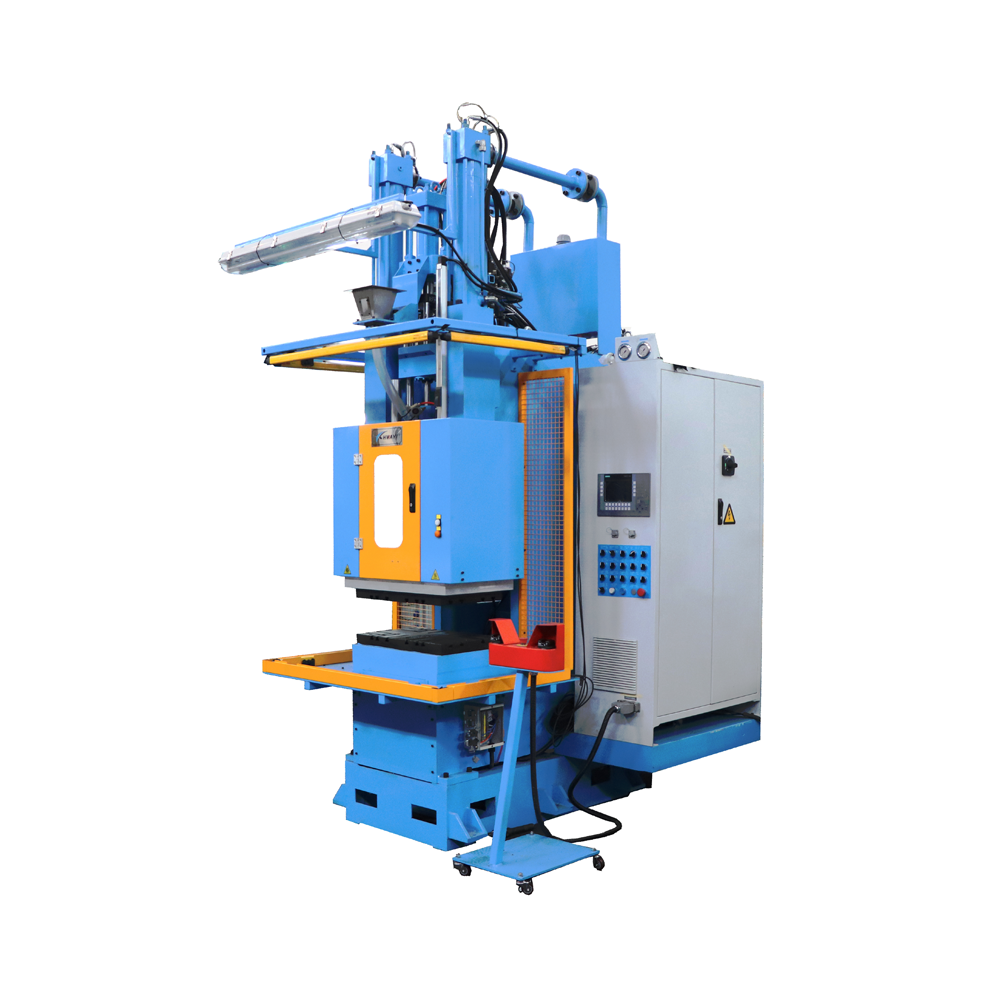
Containment: physical guards, reinforced hose routing, and pressure-rated manifolds. Use enclosure panels around hot zones and clear die set barriers that prevent access when pressure is present.
Control: hardware-level interlocks, verified pressure relief settings, and routine torque checks on fittings. Adopt redundant sensing—dual pressure transducers—so a single sensor fault triggers a safe stop rather than continued cycling.
Cognition: predictive condition monitoring and operator training that treats anomalies as spatial warnings. Implement simple trending dashboards for hydraulic pressure spikes and a mandatory lockout/tagout protocol that is short, repeatable, and enforced.
Common mistakes that keep incidents alive
Teams often assume a single fix—replace a hose, tighten a fitting—will close the chapter. That’s wishful thinking. Errors persist when maintenance records are fragmentary, when interlock bypasses are normalized, or when tooling changes are not revalidated against hydraulic setpoints. Also, do not forget tooling alignment: even a slight mismatch in a vulcanizing press can cause transient pressure peaks. —Take time to validate tooling, even during quick product changeovers.
Practical checklist for immediate action
– Verify pressure relief valves monthly and document set points.
– Route hoses away from pinch points; install abrasion guards and replace high-cycle hoses yearly.
– Fit mechanical guards on moving die sets and add physical keys that prevent manual entry during pressurization.
– Add a secondary pressure sensor with logic that forces a controlled stop if readings diverge.
– Train operators on hazard recognition; run a live drill quarterly that simulates a hydraulic rupture and the required lockout steps.
Integration notes and alternative options
When evaluating upgrades, compare traditional hydraulic-only control to electro-hydraulic hybrids that offer finer pressure control and faster fault response. If you’re installing new cells, evaluate machines that support direct safety I/O and documented fail-safes—equipment like modern transfer lines and specialized c-frame machines that report cycle and pressure data to the safety PLC reduce ambiguity. For retrofit projects, consider modular guarding and stand-alone sensor pods that don’t require a full PLC reprogram.
Advisory close: three golden rules for selection and verification
1) Verify redundancy: any single point of failure in sensing or relief must have a backup that triggers a safe stop within one cycle.
2) Measure the actual peak: instrument the press with a transient logger during production runs to capture short-duration spikes that bench tests miss.
3) Confirm human procedures: written lockout/tagout is only as strong as the practiced routine—validate by audit and surprise check.
These are practical metrics you’ll see reflected in uptime and reduced incident reports—clear numbers that justify the investment. HWAYI understands how machine design, like intelligent transfer molding and c-frame ergonomics, translates into safer, faster lines—because safety is not a sticker, it’s engineered into the cell. —Final note: steady systems win shifts.