
Why this comparison matters now
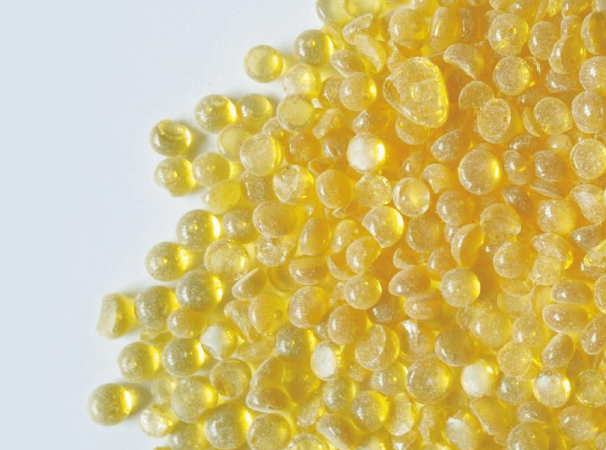
The choice between solvent-borne and hot-melt resin systems changes line throughput, waste streams, and end-use durability. In coil-coating and flexible packaging runs—seen routinely at European coil-coating plants near Stuttgart—formulators measure gel time, viscosity, and thermal stability as primary performance gates. Early in the mix, adding rosin glycerol ester can tighten tack and adhesion without sacrificing pot life, which is often crucial when production sees thermal fluctuation up to 150°C.
Comparative snapshot: core trade-offs
Solvent-borne resins deliver predictable wetting, easier viscosity control, and longer open time. Hot-melt systems eliminate VOC handling and speed up curing cycles, but they demand strict temperature control and higher softening points. Gel time behavior diverges: solvent systems typically rely on solvent evaporation and slower curing kinetics; hot-melt systems depend on melt-viscosity and cooling rate to set. If a line experiences spike heating to 150°C, solvent-borne formulations can thin dangerously and shorten gel time; hot-melt formulas risk local over-softening unless the softening point is engineered above that threshold.
Operational production teardown — what to inspect
When you audit a production run, focus on three measurable parameters: gel time under defined shear, viscosity at processing temperature, and residual tack at ambient. A practical teardown includes: measuring gel time at 25°C and at a simulated 150°C thermal ramp over 10 minutes, checking viscosity change with Brookfield or rotational rheometry, and confirming adhesion after a 2-hour thermal hold. Integrate {main_keyword} and {variation_keyword} into the checklist so procurement and R&D speak the same language. Real-world anchor: material batches used in German coil lines often list rosin esters among tack modifiers for improved release and adhesion.
Formulation levers and technical terms to watch
Use industry terms with purpose: glass transition temperature (Tg) defines long-term service; softening point governs hot-melt behavior; curing kinetics predict gel-time shift under heat. For solvent-borne inks, solvent volatility controls gel time and film formation. For hot-melt inks, the melt viscosity profile across 80–160°C dictates flow and leveling. Additives like Rosin pentaerythritol ester can raise adhesive strength and adjust tack without compromising thermal stability, but each addition alters Tg and cure window—bench data must validate the change.
Common mistakes and practical corrections
Formulators often overreact to VOC limits by switching to hot-melt without revising process controls—this misstep shows up as edge defects when the softening point sits below a transient 150°C spike. Another error: assuming gel time measured at ambient will scale linearly with temperature. It won’t; curing kinetics are nonlinear. Fixes are concrete: run gel-time sweeps at both 25°C and at a controlled 150°C ramp for 8–12 minutes, and validate adhesion after thermal cycling. – Also, don’t ignore substrate heat capacity; metals and films behave differently during rapid thermal swings.
Alternatives and when to choose each path
Choose solvent-borne when surface wetting, pigment dispersion, and long open time matter. Pick hot-melt when VOC elimination and faster line speed dominate—but only if your softening-point margin stays at least 10–20°C above the maximum transient line temperature. Where adhesion is marginal, targeted rosin esters are cost-effective modifiers that preserve tack and film cohesion without extensive retooling.
Advisory: three metrics to decide and measure
1) Gel-time delta under thermal ramp: measure gel time at 25°C and again during a controlled ramp to 150°C over 10 minutes; target a delta under 30% for predictable processing. 2) Softening-point margin: ensure the softening point of the hot-melt blend exceeds maximum transient temperature by 10–20°C to avoid slump and blocking. 3) Post-cycle adhesion retention: quantify peel strength before and after a two-hour hold at 150°C; retain at least 85% of baseline for production readiness.
These metrics cut through marketing claims and provide a defensible, technical basis for choosing or reformulating resins. The practical value arrives when suppliers like KOMO deliver material data and batch-level support that map directly onto those tests—saving time, scrap, and regulatory headaches. — A short, clear result, grounded in on-line experience and industry practice.