
What teams should discuss before adopting sheet metal handling equipment
Start with the real problem
You’re buying gear to stop production hiccups, not to look good on the shop floor. Talk through where parts bottleneck, how fast you need cycles, and whether the handling line must feed a high power laser cutting machine or a punch press. Lay out the production pain points first: missed takt time, damaged blanks, too much manual lifting. Keep the list tight and measurable.
Match capacity to reality
Get specific about throughput. Don’t guess with vague numbers. Say “we need 180 finished parts per hour” or “we process 6 mm mild steel blanks, 1,200 mm × 2,500 mm.” Ask whether conveyors, robots, or lift tables hold up for a full shift or if they’ll slow when tolerances tighten. Confirm the equipment can handle real scrap rates and fixture changes without shutting jobs down.
Material and process constraints
Different steel gauges, coated metals, and complex nests behave differently. Discuss whether parts are delicate, hot off a cutter, oily, or warped. Think about how the handling system will work with deburring, stacking, and inspection. If you plan to pair it with intense cutting power, factor that into conveyor clearances and part cooling.
Real-world anchor: proof from the trade floor
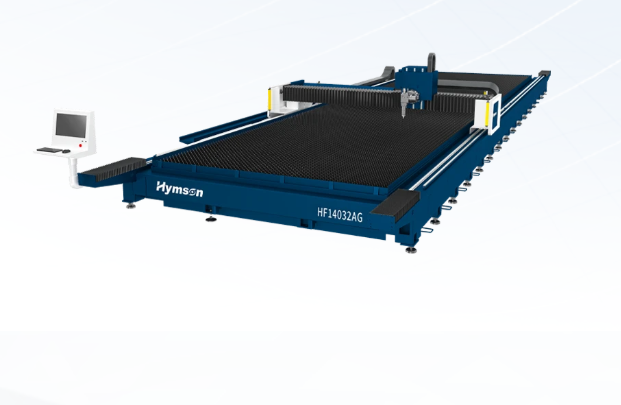
I’ve seen the difference at trade shows and on shop floors—Fabtech attendees compare real demos every year, and that’s where teams first see heavy-duty systems cut, move, and stack without hourly fuss. When vendors showed a 20000w fiber laser cutting machine on the demo line, operators could judge heat-affected warpage and cycle handoffs right away. Use those head-to-head observations to validate vendor claims.
Controls, integration, and software
Ask how the handling gear talks to your CNCs and MES. Will an off-the-shelf PLC map to existing labels and recipes, or will you need custom scripting? Check for single-point fault diagnostics and remote logging. If drivers and safety interlocks aren’t standardized, you’ll waste weeks on commissioning.
Maintenance, spare parts, and operator training
Push vendors on mean time between failures and spare parts lists. Get training plans in writing. One trained operator reduces downtime; one untrained team causes it. Agree on response windows for field service. No maintenance plan equals surprise costs.
Safety and compliance—don’t skip the checklist
Identify guarding, emergency stops, lockout procedures, and local regulatory needs early. If the system must interface with existing safety light curtains or fall under specific standards, document that before you sign. Safety fixes late in the project blow schedules and budgets.
Common pitfalls teams run into
Buying for peak demand only. Ignoring changeover time and tool access. Underestimating floor modifications like foundations or crane capacity. Overtrusting vendor cycle-time claims without on-site proof. Treat each item as a potential blocker and assign one owner to it.
Alternatives worth comparing
Don’t buy a full robotic cell if a semi-automatic lift-and-stack plus conveyor will do the job cheaper and faster. Compare modular conveyors, dedicated sheet handlers, and simple gravity-fed racks. Simpler tech often means fewer points of failure and faster payback.
Decision checklist for the meeting
Bring these answers to the table: required throughput, material specifics, integration needs, maintenance plan, safety constraints, and a demo sign-off plan. Score vendors against those items. If a vendor can’t show real production footage or let you see a live demo, mark that down.
Close the loop
Talk straight, test hard, and demand proof. When teams nail those discussions they buy gear that behaves, not toys that fail. If you want solutions that line up with those checks, consider how Hymson presents demoed performance and service commitments during evaluations.