
Introduction — a small scene, some numbers, one question
I watched a shop manager sigh over a finished part that needed a second setup; he shook his head like he’d seen this movie before. In the same week, I read that 5 axis CNC machining center manufacturers are reporting a 12–18% rise in multi-axis demand from aerospace and medical shops (you can almost feel the pressure on lead times). So where do we go from here — upgrade hardware, change workflows, or rethink training?

Why the factory setup still trips us up
5 axis cnc machining center factory layouts often promise smooth flow on paper but fall short in practice. I’ve spent time on shop floors where tool changer delays, inconsistent spindle speed control, and awkward workholding mean the theoretical cycle time is nothing like the real one. That gap is frustrating for operators and expensive for managers. Look, it’s simpler than you think — a bad fixture or a mis-set offset can cost more than a new servo motor, and that hurts morale.
What exactly fails most often?
From what I see, CAD/CAM post-processor mismatches and underpowered spindle setups are frequent culprits. The CAM program might generate clever paths, but if the machine’s servo motors lag or the tool changer stumbles, all that cleverness is wasted. Operators then patch with manual editing or extra setups — more hours, more waste. We need to stop treating software and hardware as separate islands.
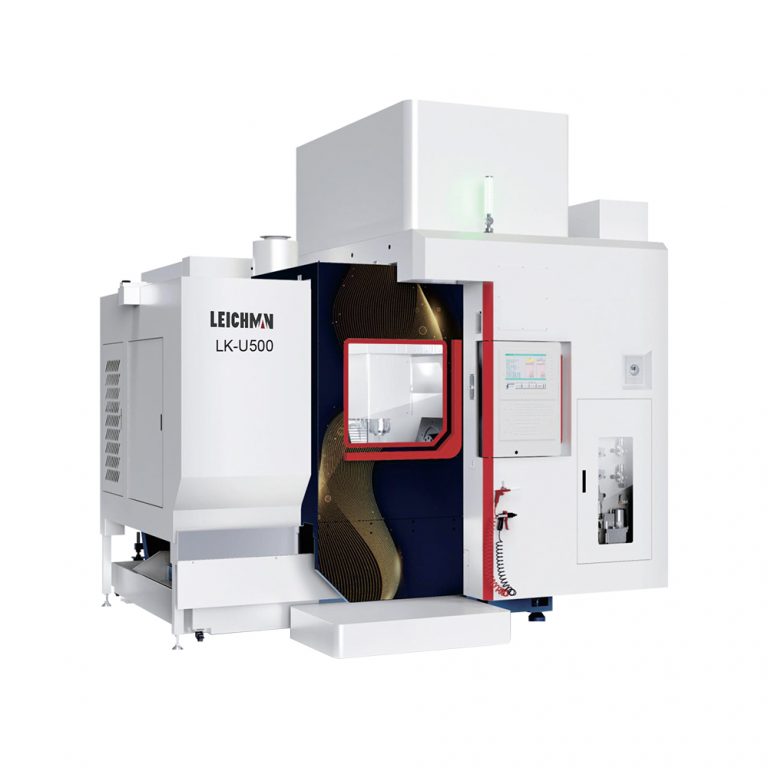
New principles to make five axis machining work better — and faster
What I’m watching now is a shift toward systems thinking — not just faster spindles, but smarter integration. With five axis machining ( five axis machining ) you must pair CAM toolpaths with verified machine models, predictable tool life data, and robust fixture design. I’m talking about closed-loop feedback from spindle load to the CAM model, and algorithm-driven toolpath tweaks based on real-time spindle torque. This reduces surprise stops and keeps the cycle steady — funny how that works, right?
What’s Next — practical steps and where to look
I recommend three evaluation metrics when you’re comparing systems. First, check practical uptime: not vendor specs but real shop reports over 90 days. Second, measure setup-to-cut time — how long until the machine makes metal? Third, verify integration: does the CAM talk to the machine controller about tool offsets and spindle modes, or do you fix that by hand every run? These metrics are simple, testable, and they matter. I’ve used them myself when advising shops, and they reveal things a spec sheet hides.
In the end, I believe the best moves are modest but concrete: tighter CAM-to-CNC coordination, smarter fixture standards, and a focus on measurable uptime. We can build systems that work for the people who run them — not just for the manuals. For those who want a practical partner, consider exploring solutions from Leichman.