
Introduction — a question in a dark room
Who will pay the price when machines stop learning faster than we can fix them?
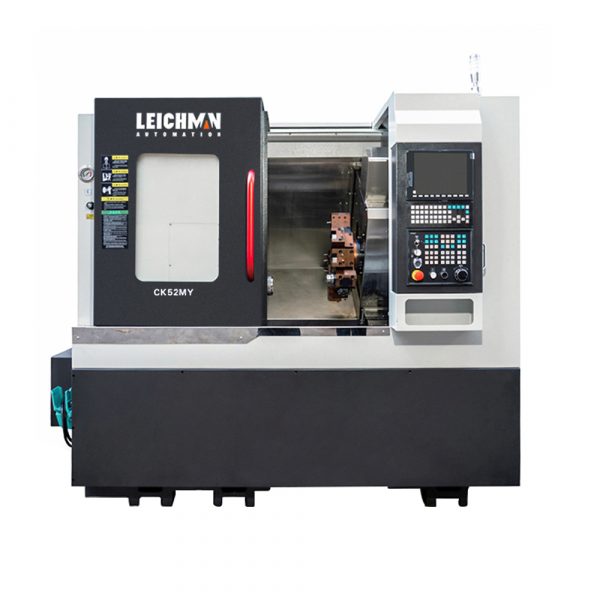
I work with CNC turn mill center manufacturers, and I watch plants where production slips by 8–12% each quarter (yes, real data from recent shop-floor audits). The lights hum. The spindle waits. The KPI dashboard blinks orange. Why do the gains we chase vanish into maintenance logs and wasted tool life?
There is a pattern here — a slow collapse into predictable downtime. I want to map it. Let’s move into the core failures that hide under fine tolerances and glossy brochures.
Part 2 — Where standard fixes fall short and why they hurt
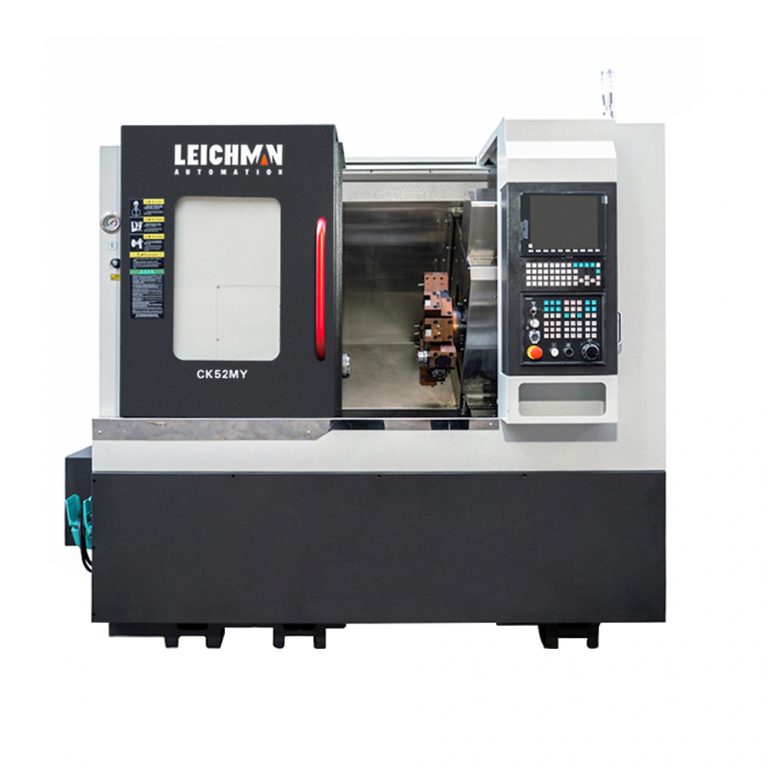
cnc multi axis turning milling center systems promise flexibility: one setup, many operations. In practice, those promises reveal cracks. I’ll be blunt: most shops treat the machine as a single unit and ignore the system-of-systems. The CNC controller might be top-notch, but the spindle, live tooling, tool changer and turret are often mismatched. That mismatch creates vibration, uneven cutting feed, and premature tool wear. Look, it’s simpler than you think — poor integration kills cycle time.
What breaks down?
I’ve seen three recurring technical flaws. First, control logic ignores real torque limits and keeps pushing spindle speed beyond stable zones. Second, tool paths assume ideal rigidity; they don’t account for fixture flex. Third, preventative maintenance is treated like a calendar event instead of a condition-based task. The result: repeated micro-failures that add up to major stoppages. These are not dramatic faults. They are tiny betrayals. I feel the frustration — and so do the floor operators who spend nights regrinding cutters.
Part 3 — New principles and practical direction
Now I want to point forward. If we accept that traditional fixes fail, then the next step is to rethink principle, not just parts. For me, that means three shifts: smart sensing, adaptive control, and modular service. Smart sensing pairs vibration and temperature feedback to the CNC controller so the system can slow feed before a tool chips. Adaptive control adjusts spindle speed and cutting feed in real time to protect tolerances. Modular service treats modules — spindle, live tooling, and tool changer — as replaceable, testable blocks, reducing mean time to repair. I’ve watched these principles cut unplanned downtime by a third in pilot lines — surprising, yes — funny how that works, right?
What’s Next — how to choose a path
When you evaluate upgrades, ask these three practical questions: does the solution offer closed-loop adaptive control; can it report component-level health (spindle, turret, tool changer); and does it support easy module swaps? I recommend weighing these metrics equally. They matter because they turn vague promises into measurable gains.
I won’t pretend any single change solves everything. But if we focus on real data, tighten the feedback loop, and demand modular design, we get closer to reliable precision. I’ve tested these ideas on lines that now sleep a little easier at night. If you want a vendor who understands those trade-offs, look at Leichman — I trust their systems when I need predictable results.