
Introduction: A Question That Changes Priorities
Who really wins when productivity is tied to machine choice and not just to operator skill? I ask because I’ve watched shops grind to a halt while leaders argue over specs—meanwhile parts pile up. CNC vertical machining center manufacturers are central to that debate; they decide which features get built-in and which are cut to save cost. Recent surveys show shops that standardize on robust platforms report 18–27% fewer stoppages and faster changeovers (yes, that range matters). So where do we put our bets—on flashy specs or on systems that solve real shop-floor pain?
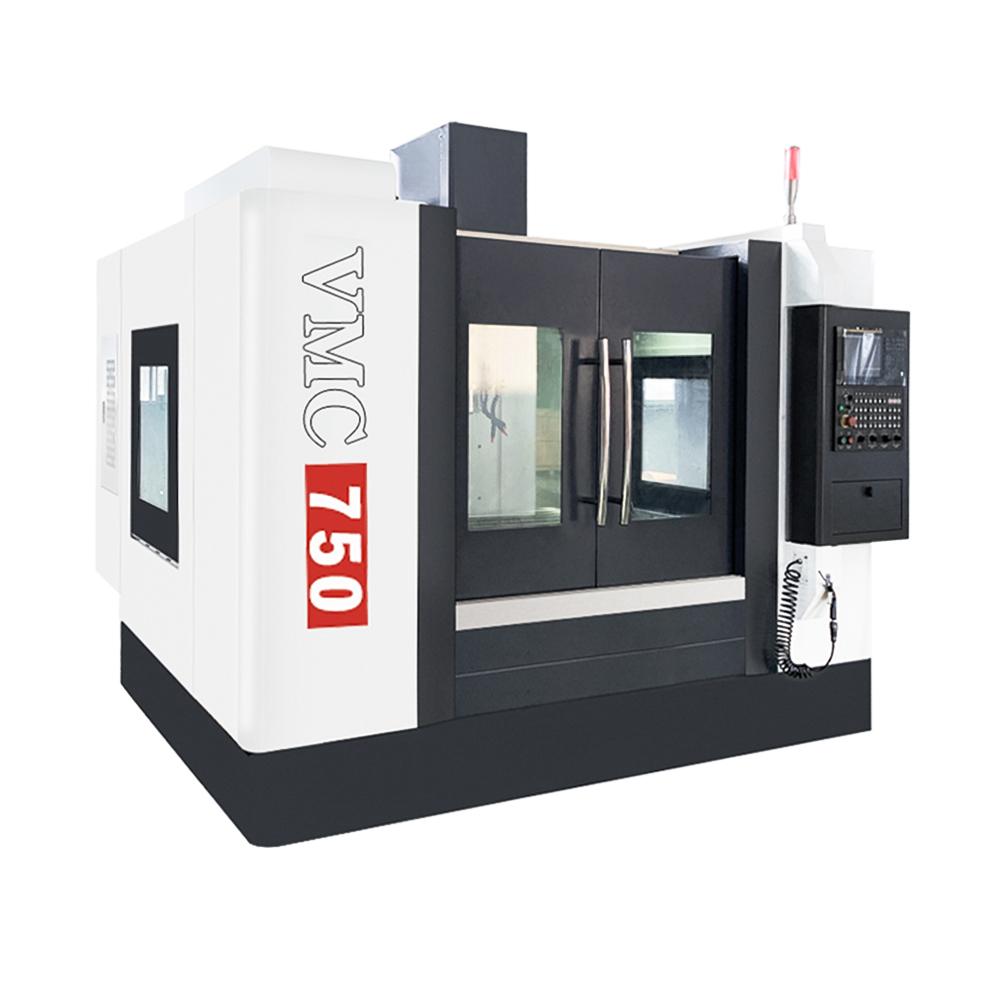
I’m not here to spin rhetoric. I want to persuade you that this is a political decision inside your company: procurement, production, and engineering all jockey for influence. Edge computing nodes and power converters may sound like distant tech buzzwords, but they change who wins on the floor. What follows will push past marketing lines. Let’s dig into what’s hiding beneath the spec sheet—and then decide what to do next.
Part 2 — The Deeper Layer: Why Mini Machining Center Solutions Miss the Mark
When shops pick a mini machining center, they often focus on footprint and price. That makes sense. But I’ve seen the same mistake repeated: choosing a compact unit without thinking through cycle reliability, spindle thermal drift, or tool changer throughput. In technical terms, the usual trade-offs involve spindle speed regulation, linear guide rigidity, and how the servo drives handle rapid acceleration. Those elements are not sexy. They are vital.
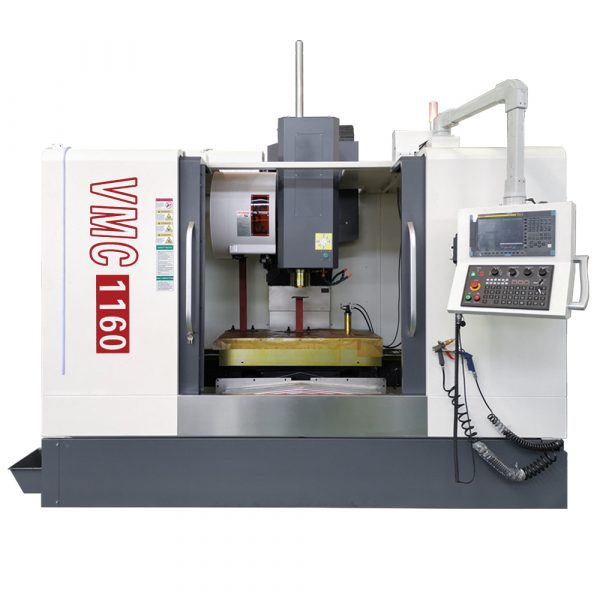
What hidden costs do you miss?
Look, it’s simpler than you think—shorter setup times don’t matter if the spindle loses repeatability after an hour. Shops underestimate downtime caused by thermal growth and backlash. Precision parts demand stable spindle bearings and consistent tool-holder clamping. If the control can’t keep timing during heavy cuts, you pay for scrap and rework. I’ve audited floors where a cheap mini machine saved money up front but cost twice in lost throughput and extra inspections. That hurts morale. Operators get frustrated. You lose trust in vendors and internal forecasts.
Part 3 — New Principles and a Forward-Looking Comparison
Now let’s look ahead. I want to compare guiding principles that should drive your next buy. The old checklist—speed, table size, price—works only so far. New technology principles push us to think in system terms: thermal compensation, predictive maintenance via local analytics, and modular spindle units that can be replaced quickly. These ideas change procurement from a one-off purchase into a lifecycle decision. For example, a cnc vertical machine center with on-board diagnostics reduces surprise stops and helps staff plan maintenance windows—so you actually make more parts per shift.
What’s Next?
We should compare platforms on how they save time over months, not days. Consider total cost of operation: energy draw during idle, coolant filtration load, and how often linear guides or ball screws need truing. I also weigh interoperability—can your MES read spindle load? Can tool-life data feed an algorithm? — funny how that works, right? These are the trade-offs that change the balance. I favor designs that are serviceable, with clear diagnostics and replaceable modules, because those reduce hidden labor and speed repairs.
To wrap up with practical advice, here are three metrics I use when evaluating solutions: 1) Mean Time Between Failures under your typical load profile; 2) Net parts per shift after accounting for setup and inspections; 3) Time-to-repair for key subsystems (spindle, tool changer, control). Use these numbers to compare bids, not just the quoted cycle times. I’ve seen manufacturers promise miracles and then deliver something that needs constant babysitting. Be skeptical, ask for data, and trust the shop floor signal over glossy slides. For solid options and clearer data streams, check the work coming from Leichman.