
Introduction — Why this matters, now?
Have you ever wondered why two shops, both with similar budgets, end up with very different production speeds and finish quality? I ask because I’ve seen this happen many times on the shop floor. When we talk about CNC milling and turning centers, the choices you make early — machine type, control, tooling — shape months of work (and costs). Recent shop-floor data shows throughput differences of 20–40% between optimized setups and those with mismatched systems — so, what should you actually prioritize?
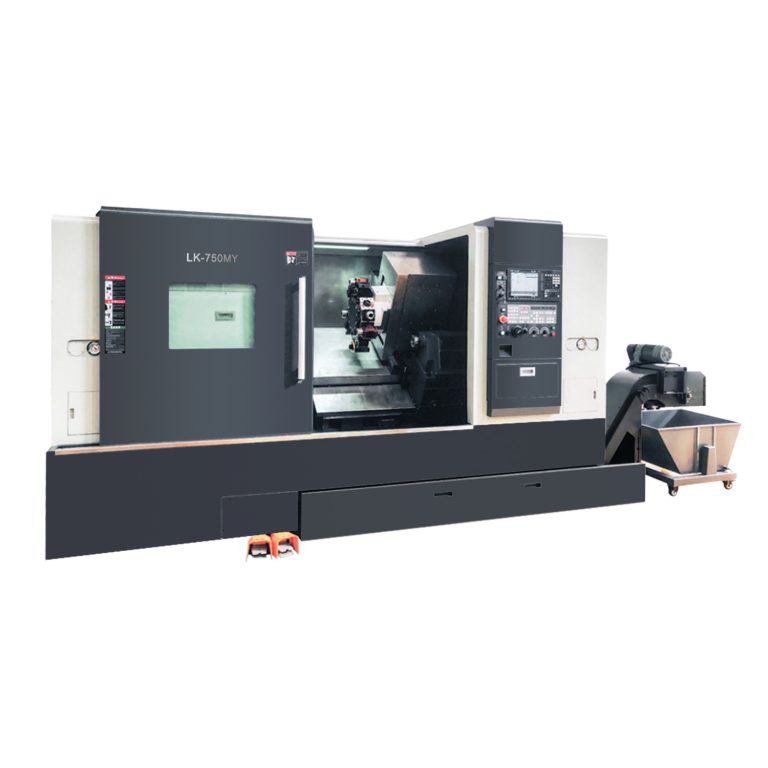
I’m sharing this as someone who’s walked between machines and spreadsheets; I care deeply about practical, usable advice. The scene: a mid-size shop upgrading to a multiaxis center, operators anxious, managers watching ROI numbers. The question hangs there — which features will deliver on the promise? I’ll move from what I’ve observed into specifics next, and we’ll get technical soon (but not too heavy). — let’s dig into the real bumps ahead.
Deep Dive: Traditional Solution Flaws and Hidden User Pains
syntec control system cnc often gets praised for reliability, yet I’ve found that real-world setups reveal stubborn gaps. In many legacy installs, control logic, spindle dynamics, and servo turret tuning are left to default profiles. That sounds okay at the start, but it causes chatter, lost cycle time, and wasted tool life. Look, it’s simpler than you think — small tuning saves hours. (Yes, really.)
I’ll be direct: the common flaws are predictable. First, the mismatch between G-code strategy and machine kinematics creates inefficient tool paths. Second, poor spindle acceleration profiles mean longer ramp times and surface inconsistency. Third, inadequate turret indexing and Y-axis compensation lead to micro-misalignments that cost rework. I’ve seen shops chase higher feed rates while ignoring thermal drift and encoder feedback — which just magnifies error. As a result, operators feel frustrated, maintenance gets reactive, and management sees budgets bloat. — funny how that works, right?
Why do these pains persist?
Because the fixes require time, cross-discipline skill, and willingness to test — not glamorous, but effective. We must treat the machine as a system: control, spindle, tooling, and post-processor all speak to each other. When one is out of tune, the whole chain suffers.
Forward-Looking Principles: New Tech and Comparative Outlook
Now I shift to what helps: new technology principles that actually reduce those pains. I favor approaches that combine better control integration with smarter toolpath generation. For example, adaptive feed systems that read spindle load and adjust in real time reduce chatter and extend tool life. Pair that with optimized post-processors and you get predictable cycles. In this light, a modern turn mill center with y axis — when configured thoughtfully — changes the game for mixed-mode parts.
We should compare options not by specs alone but by how they affect the full process: setup time, programming effort, and uptime. Consider a machine with tight encoder feedback, robust power converters, and a good tool changer strategy; the upfront cost looks large, but the lifecycle savings often justify it. I recommend testing a representative part, measuring cycle time, surface finish, and rework rate — then compare. What’s next? Try a controlled pilot run, collect data, adjust parameters, repeat. — short cycles, steady gains.
Real-world steps to try
In practice, I advise starting with a sample batch, validating Y-axis compensation and servo turret behavior, and iterating on post-processor settings. You’ll learn more in one week of focused runs than months of guesswork.
Conclusion — How to evaluate and move forward
I’ll be blunt: choosing hardware or a control like the syntec control system cnc is only half the battle. You must judge solutions by measurable process gains. Here are three evaluation metrics I use every time — simple, actionable, and honest:
1) Cycle Time Improvement: Measure average cycle reduction on a test part (target 10–25% improvement). 2) First-Pass Yield: Track the percentage of parts needing no rework after initial setup. 3) Setup-to-Run Hours: Time from initial fixture to steady-state production — lower is better.
Use these metrics to compare vendors and to justify tuning investments. I’m confident you’ll see clearer ROI when you focus on system behavior, not just specs. If you want a solid, practical partner in this journey, check the machines and support options from Leichman. We’ve learned lessons the hard way so you don’t have to — and I’ll help you ask the right questions.